News —
Zero-Defect Production: Why Proper Marking Starts Right at the Beginning of the Production Process
Zero-defect production does not begin with the final inspection. The earlier a component can be uniquely identified, the easier it is to track process and quality data throughout the manufacturing process. This also changes the role of industrial marking: What was once a final marking step is increasingly becoming an integral part of process and quality assurance.
The goal of zero-defect production is not to find as many defects as possible at the end of a production process. The key is to detect deviations as early as possible—or to prevent them entirely. To achieve this, it can be beneficial to uniquely mark a component while it is still a semi-finished product.
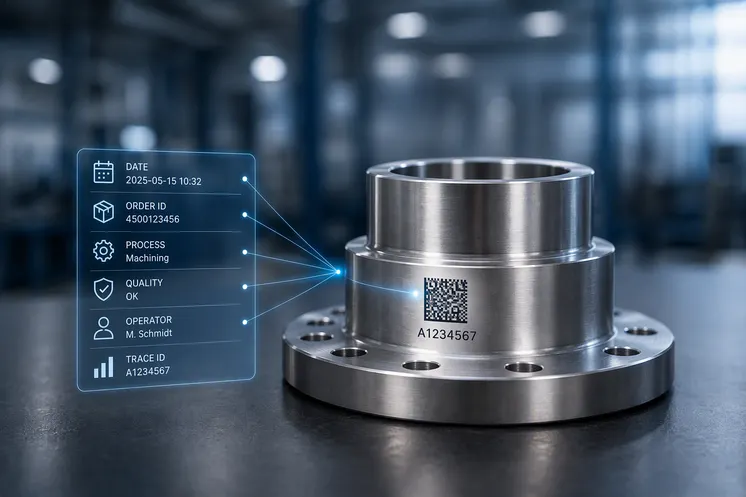
Traditionally, marking is often associated only with the finished product: After machining, assembly, and inspection, a component is assigned, for example, a serial number, type information, or a machine-readable code, and then leaves production. However, for end-to-end traceability, identification can begin much earlier. Simply marking a semi-finished product or semi-finished item makes it possible to uniquely identify the component at subsequent stages within the manufacturing process. The code serves as the workpiece’s ID. At each subsequent production or inspection step, this identity can be read and linked to the information generated there: What machining operations were performed? What parameters were used? What measurement values were recorded? Which test was passed? The marking thus serves as a common thread throughout production. It is not only the finished product that becomes traceable; its entire production process can also be traced, and process deviations can be assigned to the respective component and production step.
The information required during manufacturing does not necessarily have to be identical to that on the final product. Early marking can initially serve for internal identification and, after defined machining and inspection steps, be supplemented or replaced by a final marking. Depending on the material, marking method, and subsequent machining steps, this can also take place at the same location. For example, a marking initially used for the production process can later be replaced by the final product marking. This is particularly relevant for products that do not receive a final paint finish or coating. For in-process marking, it is therefore less critical whether the same physical code remains consistent throughout the entire manufacturing process. What is crucial is that the component’s identity and the associated quality and process information are unambiguously preserved during the transition from one marking to the next. This is precisely where marking becomes relevant for zero-defect production: quality information can be assigned not only to a batch or a production order, but also to the individual component and its respective manufacturing steps.
Why is marking quality crucial for zero-defect production?
The more production and quality processes depend on unambiguous component identification, the more important the quality of the marking itself becomes. A code that cannot be reliably read is not just a visual defect; it can prevent process or inspection data from being unambiguously assigned or cause a component to be processed incorrectly at a subsequent station. As a result, even a technically flawless component can become a problem. If the marking does not meet the required quality criteria, additional inspections and rework may be necessary. In the worst-case scenario, this results in scrap. The later such an error is detected within the value chain, the more processing, inspection, or assembly steps may already have been applied to the component. For zero-defect manufacturing, it is therefore not enough to consider only the quality of the component itself. Its unambiguous and reliable identifiability also becomes a quality characteristic. This raises several questions regarding the marking process:
• Is the correct component marked with the correct information?
• Is the code reliably readable at the relevant process stations?
• Does the marking quality remain reproducible across production lots and shifts?
• Are deviations detected before further value is added?
• Is the unique assignment maintained even if an internal process marking is later replaced by the final product marking?
Especially when it comes to machine-readable codes, the statement “the code can be read” does not go far enough. A single successful read does not necessarily indicate whether the marking achieves reproducible quality under defined production conditions. This is precisely where ISO/IEC 29158:2025 for Direct Part Marking comes into play. The second edition, published in 2025, establishes a methodology for quality testing of directly applied codes. Among other things, it takes into account defined lighting conditions, image capture, and parameters for evaluating symbol quality. This allows for a more objective assessment of marking quality. This is particularly relevant when codes must be reliably read not only immediately after marking but also at subsequent stations. For manufacturing companies, this shifts the focus from simply generating a mark to a controlled marking process: The correct data must be assigned to the correct component, marked in a reproducible manner, and, where the application requires it, subsequently verified. Especially for manufacturers with defined traceability and compliance requirements, reproducible marking quality thus becomes an integral part of process reliability.
Zero Defect means preventing errors before they incur costs
This development aligns with an overarching trend in industrial quality assurance. Quality is increasingly monitored directly within the production process rather than being checked only at the end. Detecting marking errors early allows companies to reduce rework and prevent incorrectly identified components from proceeding through further value-adding process steps. The European openZDM project has pursued this approach in various industrial pilot applications. Process data, digital technologies, AI, and non-destructive inspection systems were used to monitor critical quality characteristics and detect potential problems earlier, before they result in rework or scrap. Applied to industrial marking, this means that an additional final inspection alone does not automatically make a marking process more reliable. The key is to prevent or detect potential errors as close as possible to where they occur. This applies not only to laser parameters. Material and surface texture, focus position, and component orientation all influence the physical marking result. Production data and standardized processes also determine whether the correct marking is applied to the correct component. The more closely marking and quality control are integrated into the production process, the sooner deviations can be detected and follow-up costs avoided. When it comes to the permanent marking of industrial components, this means that not only are the requirements for legibility increasing, but also those for reproducibility and unambiguous data assignment.
Different Industries, Similar Quality Requirements
What these requirements look like in practice depends on the component, material, and manufacturing environment. In many industrial applications, however, the same fundamental question arises: How can we ensure that the correct workpiece is marked reproducibly with the correct information and the required marking quality? In the automotive, rail, and supplier industries, for example, components often undergo multiple machining and inspection steps. Unambiguous identification makes it possible to assign quality and process information to the respective workpiece. At the same time, high production volumes and short production cycles place high demands on reproducible processes. In mechanical engineering and among manufacturers of industrial components, on the other hand, changing production runs, varying workpiece sizes, and variable marking content may take center stage. In addition to static product information, serial numbers or Data Matrix codes—which are generated individually for each component—are required, for example. For electronic components and plastic parts, on the other hand, small marking areas, sensitive surfaces, and high contrast requirements can play a significant role. While the specific applications differ, they all share the need for a controllable marking process.
Marking quality is determined by the process, not by the laser alone
Therefore, a high-performance laser alone is not sufficient to ensure reproducible marking. The material, laser parameters, marking data, component positioning, and the marking process sequence all collectively influence the result. For standardized industrial marking tasks, Trotec relies on MOPA fiber laser technology in its SpeedMarker series. Thanks to the variable pulse duration, the laser process can be specifically adapted to different metals and plastics. Possible applications include, for example, high-contrast markings on plastics and black markings on anodized aluminum. For Zero Defect, this flexibility is particularly important because what matters most for each material is not maximum laser power, but a stable and reproducible result. The laser source is only one part of the entire process.
The Right Data Is Also Key to Marking Quality
Even a physically flawless mark can be a defect if it contains the wrong information. Especially with customized product data such as serial numbers or Data Matrix codes, it is therefore essential to ensure that the correct data is assigned to the correct component. This makes the software an integral part of process reliability. The Ruby® laser software supports the digital marking workflow and helps ensure that marking data and recurring processes are provided in a controlled manner. This broadens the concept of marking quality: A good marking must not only be high-contrast and legible; it must also be produced on the correct component, in the correct position, and with the correct information.
The Marking Station as a Controlled Quality Step
This is precisely where industrial galvo systems such as the SpeedMarker series come into play. These systems combine a fast galvo marking process with software-based control of the marking workflow. For Zero Defect, it is less important whether the marking station is physically part of an automated production line. What matters is the controlled handoff between the manufacturing process and marking. The ideal workflow might look like this, for example:
Identify component → Assign production data → Position workpiece → Apply marking → Check marking quality → Release component for the next process step
The fewer of these steps that depend on individual manual decisions, the easier it is to standardize recurring processes. This is precisely the approach of a Trotec ecosystem for industrial marking: lasers, software, component positioning, and handling are not viewed as independent components, but as integral parts of a reproducible marking process. This means that productivity cannot be increased solely through higher marking speeds. The time before and after the actual laser marking is also taken into account. This is relevant to the “zero-defect” philosophy: A stable process must be reproducible, cost-effective, and practical for the specific production situation.
From Marking Technology to Quality Strategy
Industrial marking is thus evolving from an isolated processing task into a defined quality control step. The component can be assigned an identity as early as the semi-finished stage, linked to production and inspection data via this identity, and later receive its final product marking. Software supports the correct assignment of dynamic data, while a controlled laser process ensures reproducible marking results. For manufacturing companies, this also changes the criteria used to select a marking system. In addition to cycle time and marking speed, reproducibility, material and process control, correct data assignment, positioning, and quality control are taking center stage. The decisive factor in industrial marking is therefore not merely how good it looks immediately after marking. What matters is whether it reliably fulfills its function in the intended production process. Zero Defect thus also changes the perspective on laser marking: a simple marking task becomes a controlled quality process.